The load slips or drops
Shape, hardness and material are chosen for your surface (smooth, oily, rough) and your weight.
Vacuum handling · Manufacturer
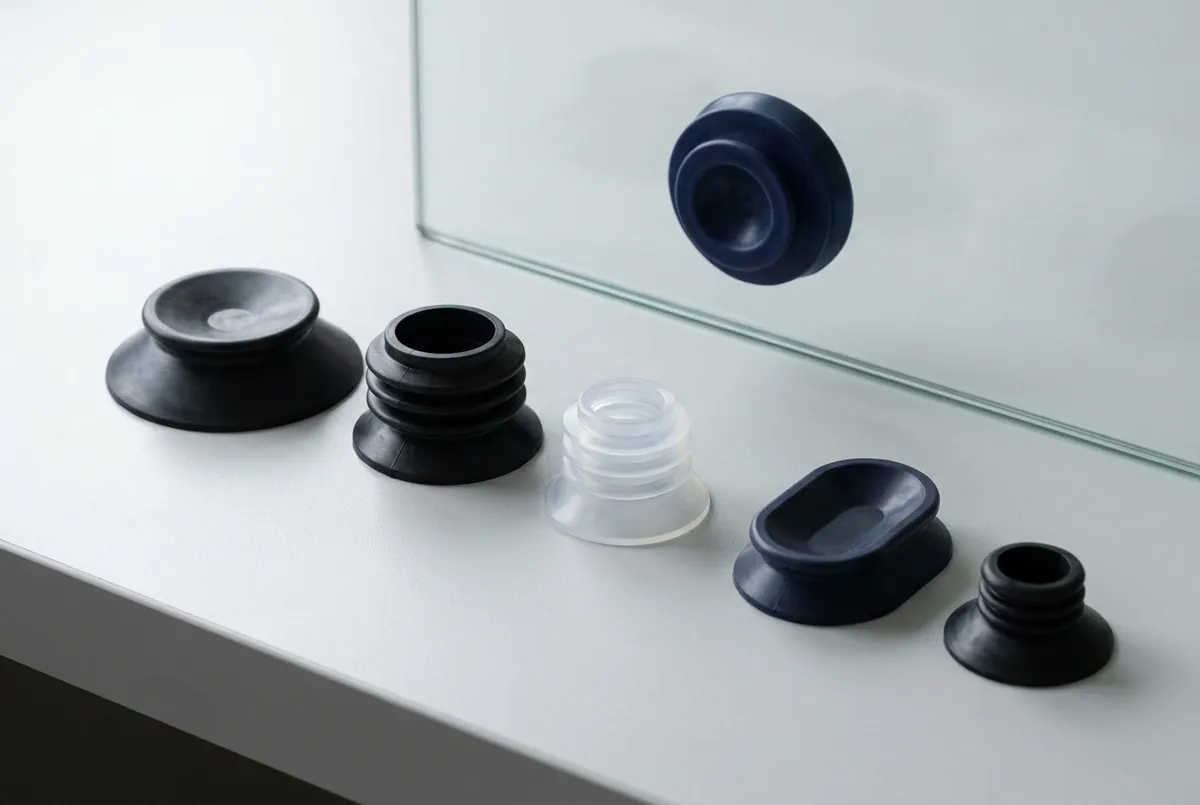
Custom vacuum cups for packaging machines, robot grippers and vacuum lifting equipment — flat, bellows and oval, with or without bonded metal inserts. Produced to your drawing or sample, in a compound we formulate for the surface the cup has to grip.
Do you recognise any of these? Most are solved with the right material, section or tooling. Tell us which one is yours and send the drawing, a sample or the part that failed.
Shape, hardness and material are chosen for your surface (smooth, oily, rough) and your weight.
We can make cups in silicone and in compounds formulated not to leave marks on the surface you handle.
A compound resistant to abrasion and to the cycle of your process, with a section that spreads the wear.
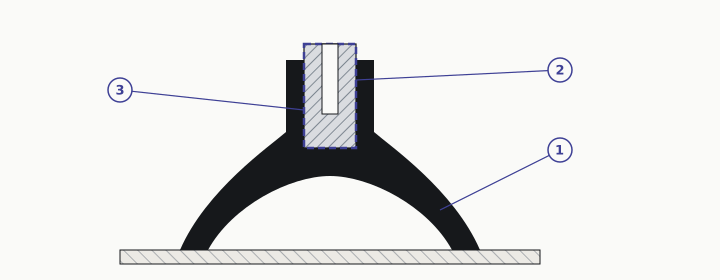
We make the geometry and the fixing your equipment needs, including a metal insert bonded during vulcanisation.
Made to order in Curitiba, with an engineer who answers your questions. Lot size agreed per part.
Each new cup is made in its own mold, and the minimum quantity is agreed per part. We supply companies only — we do not sell single cups or small quantities to end users.
Silicone suction cups for packaging machines: carton erecting, pick-and-place of pouches, trays and blanks. Light, non-marking compounds where the cup touches printed board or film, and a hardness chosen for the cycle rate rather than taken from a standard grade.
Suction cups for robot grippers, produced under the integrator's own part number. Bellows cups where the gripper needs compliance on uneven parts, and cups with a bonded metal insert where the cup mounts directly onto the vacuum fitting.
Flat and oval pads for lifting glass, sheet metal and panels. Larger diameters are compression molded. The compound is chosen for grip on the real surface — oily, wet, painted or polished — and for the loads the lifter is rated to carry.
If the cup you use today is imported, send us a sample. We reproduce the geometry in a dedicated mold, develop a compound for your surface and supply it in series from Brazil, with every compound batch checked before release and the approved formulation frozen.
A suction cup has to do three things that pull against each other: seal against an imperfect surface, hold the load without slipping, and release the part without leaving a trace of itself behind.
The first two are geometry and hardness. The third is compound chemistry, and it is where most suction cups fail commercially rather than mechanically.
A cup that leaves a mark on a painted panel, a polished sheet, a glass pane or a printed carton produces a rejected workpiece — not a rejected cup. Marking comes from plasticiser migration and from filler transfer at the contact face, both of which are formulation problems. Because we mix our own compounds, we can adjust the formulation against the surface rather than choosing the least bad option from a catalogue.
A soft compound seals well on rough or curved surfaces but deforms under shear and lets the load slip. A hard compound holds shear but seals poorly. The working answer is usually a specific hardness for a specific surface, which is why we produce across 25 to 90 Shore A rather than offering a standard grade.
Cups working near ovens, in cold stores, in oily press shops or under continuous cycling all age differently. Temperature range, oil contact and cycle count change the material choice before the geometry is even discussed.
| Type | Used for |
|---|---|
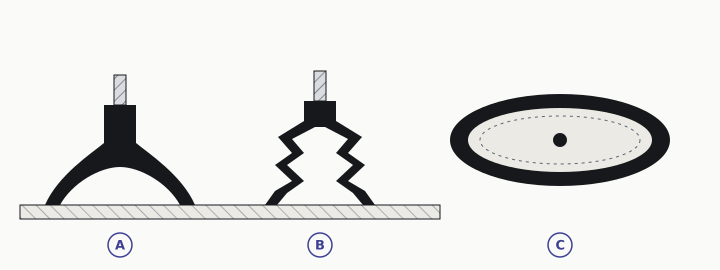
| Flat suction cups | Smooth, rigid surfaces — glass, sheet metal, panels |
| Bellows cups | Uneven or angled surfaces, and where vertical compliance is needed |
| Oval and rectangular pads | Long or narrow workpieces, profile handling |
| Cups with bonded metal inserts | Metal insert vulcanised into the cup, for direct mounting on the vacuum fitting |
| Rubber-to-plastic assemblies | Where the fitting is a molded plastic part integrated into the cup |
| Sealing rings and mounting gaskets | Interface between cup and vacuum fitting |
| Family | Chosen when |
|---|---|
| VMQ — silicone | Wide temperature range, low marking risk, clean environments |
| NBR — nitrile | Oil and grease contact, press shops, machined parts |
| NR — natural rubber | High grip and resilience, general handling |
| EPDM | Outdoor, ozone and weather exposure |
| CR — chloroprene | Moderate oil combined with weather resistance |
Hardness 25–90 Shore A. Colour to requirement, including light and non-marking compounds. Injection molded, or compression molded for larger diameters and short runs.
| 1 · Drawing or sample | We comment on manufacturability and material before any tooling is committed. |
|---|---|
| 2 · Compound | Formulated in-house for the surface, the temperature range and the media the cup will meet. |
| 3 · Tooling | Built with partner toolmakers. Existing tooling can often be transferred and requalified, usually faster and cheaper than starting from a drawing. |
| 4 · Samples | Supplied with a dimensional report. |
| 5 · Series | Rheometer curve and hardness checked on every compound batch. Once approved, the formulation is frozen: no change without prior written notification. |
Compounding is inside our ISO 9001:2015 certified scope. More on the plant in Capabilities and on batch control in Quality.
To quote a suction cup we need:
Each new cup is made in its own mold, and the minimum quantity is agreed per part. We supply companies only — not single cups or small quantities for end users. Enquiries go directly to one of the partners — see Company.