The door or lid takes too much force to close
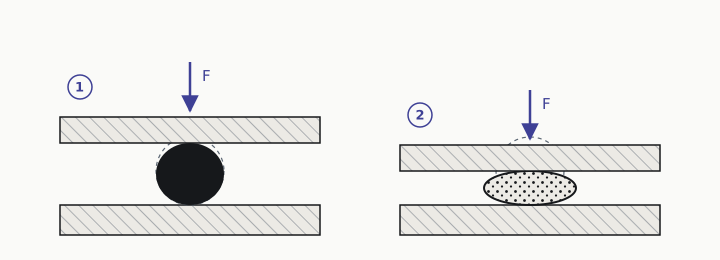
A sponge profile compresses with little force and fills the gap. We adjust density and section to the closing force your design allows.
Extrusion · Profiles, cords and tubing
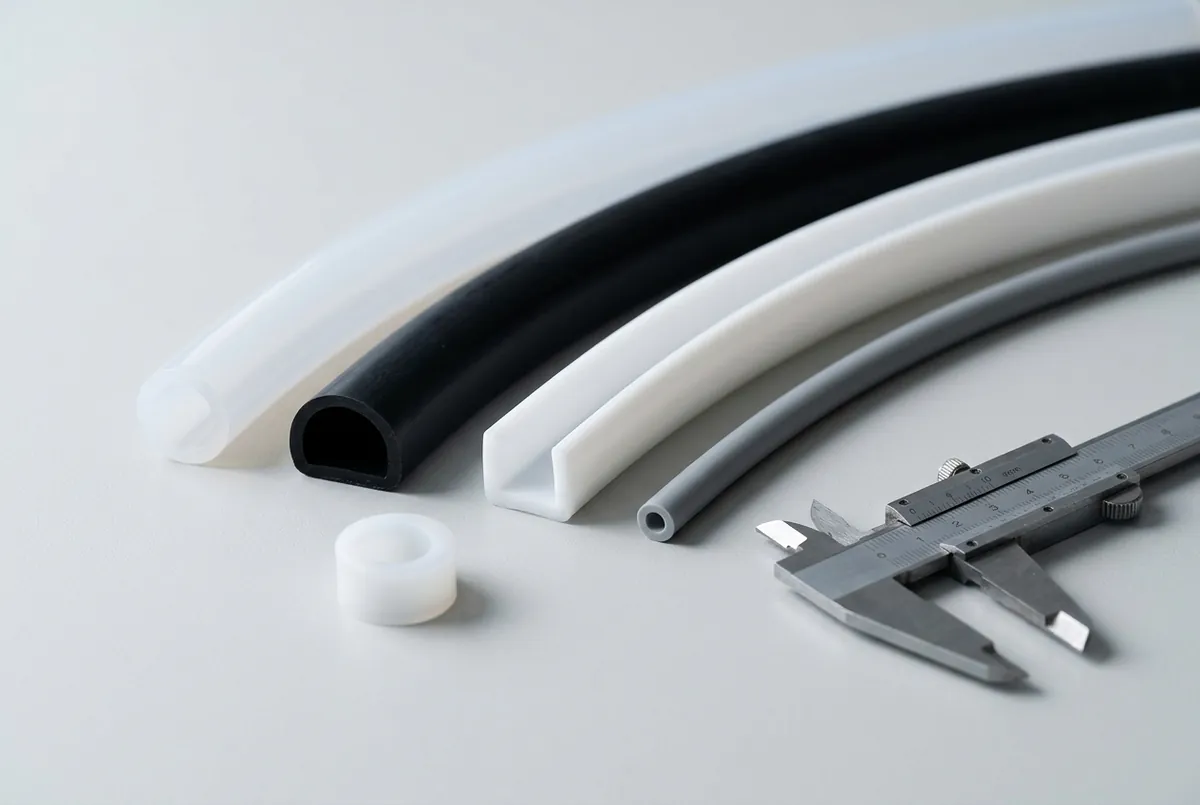
Solid and sponge profiles, cords and tubing in silicone, EPDM and NBR, extruded to your drawing on three lines with hot-air vulcanisation and cut to length with 100% inline inspection. The compound is mixed in our own plant, so the profile and the material are developed together.
We supply companies only, in production quantities. Minimum length is set by the profile, typically from 200 m. We do not sell by the metre to end consumers.
Do you recognise any of these? Most are solved with the right material, section or tooling. Tell us which one is yours and send the drawing, a sample or the part that failed.
A sponge profile compresses with little force and fills the gap. We adjust density and section to the closing force your design allows.
Permanent set comes from a compound that does not suit the temperature or the time under compression. We choose compound and hardness for your duty, and change the rubber or move to silicone when needed.
We extrude the section from your drawing. An extrusion die usually costs far less than an injection mold, so a custom profile is often within reach.
Inside diameter and wall to your drawing, cut to length or continuous, from 200 m.
For sun, ozone and weather we use silicone or EPDM. The compound is mixed here, so we tune it to your application.
Continuous series for years, including for export, on three extrusion lines. We schedule supply with you.
Sealing, guide and protection profiles in solid silicone, EPDM or NBR, produced to the section on your drawing.
Sponge silicone profiles, EPDM sponge seal profiles and sponge cords for seals that must close with low force — doors, covers, housings and enclosures.
Silicone and rubber tubing for fluid and air transfer and for protective sleeves, in the bore and wall on your drawing.
Profiles and tubes cut to length on automated equipment, with every cut part passing 100% inline inspection before packing.
A seal that takes a permanent set stops pushing back against the door, cover or housing it closes, and starts to leak long before it looks worn. Compression set is decided by the compound and by its cure, which is why we formulate, extrude and vulcanise in the same plant.
A sponge section closes with a fraction of the force a solid section needs and fills uneven gaps, so it is the usual choice for doors, covers and enclosures with light clamping. A solid section holds its shape, resists abrasion and carries load. The choice is made against the closing force available in your design, not against a catalogue.
How much a section swells as it leaves the die follows the viscosity of the compound. A profile that drifts in size from batch to batch usually has a compound problem, not a die problem. We check every compound batch on the rheometer and for hardness before it reaches the extruder, measure the diameter continuously while the line runs, and inspect every cut part inline.
Silicone for wide temperature ranges and clean environments, EPDM for weather, ozone, UV, hot water and steam, NBR where oil and fuel are present. Temperature, media and outdoor exposure decide the family before the section is drawn.
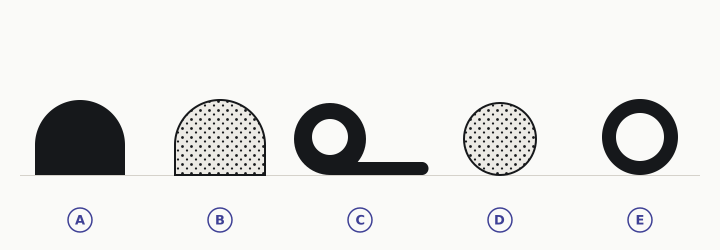
Any extruded section in silicone or rubber that fits our lines. Send a drawing, a sample, or a short length of the profile you use today: we have the die made for your section, develop the compound and supply a sample length for approval before series production.
Our extrusion lines already run continuous series for export to mining equipment manufacturers, and seals for outdoor housings that have to stay closed for years against water, dust and temperature cycling. Where an application requires food-contact compliance, the compound is qualified by an accredited laboratory as part of the development.
More on the plant in Capabilities and on batch control in Quality.
Sponge and solid sections can be produced in the same family of compound. Colour to requirement, including light silicone.
| Material | Form | Chosen for |
|---|---|---|
| Silicone (VMQ) | Solid and sponge | Wide temperature range, low compression set, clean environments, light colours |
| EPDM | Solid and sponge | Weather, ozone, UV, hot water and steam — outdoor housings and enclosures |
| NBR | Solid | Oils, fuels and hydrocarbons |
| Item | Specification | Note |
|---|---|---|
| Extrusion lines | 3 | Hot-air tunnel vulcanisation |
| Hardness | 25–90 Shore A | Set by the compound for each application |
| Tolerances | To customer drawing | Tightest on functional dimensions |
| Dimensional control | Diameter measured continuously during extrusion | Cut parts: 100% automated inline inspection |
| Supply form | Continuous lengths or cut to length | Cutting on automated equipment |
| Compound control | Rheometer curve and hardness on every batch | Approved formulation frozen |
| Minimum quantity | Set by the profile, typically from 200 m | Each new section needs its own die |
To quote an extruded profile we need:
We supply companies only. Minimum length is set by the profile, typically from 200 m. Enquiries go directly to one of the partners — see Company.